Comprehensive Food Factory Stores Area Refurbishment
Scope of Work: Full refurbishment of an existing stores area
Key Deliverables: Hygienic stainless steel kerbing, EHEDG-compliant drainage system, stainless steel handrails, Foodcrete resin flooring,
Project Overview
KDH Projects, specialists in delivering construction solutions within live food production environments, was commissioned to refurbish an existing stores area at a leading food manufacturing facility. Our expertise in working within live production sites ensures that food safety remains uncompromised throughout the entire project lifecycle.
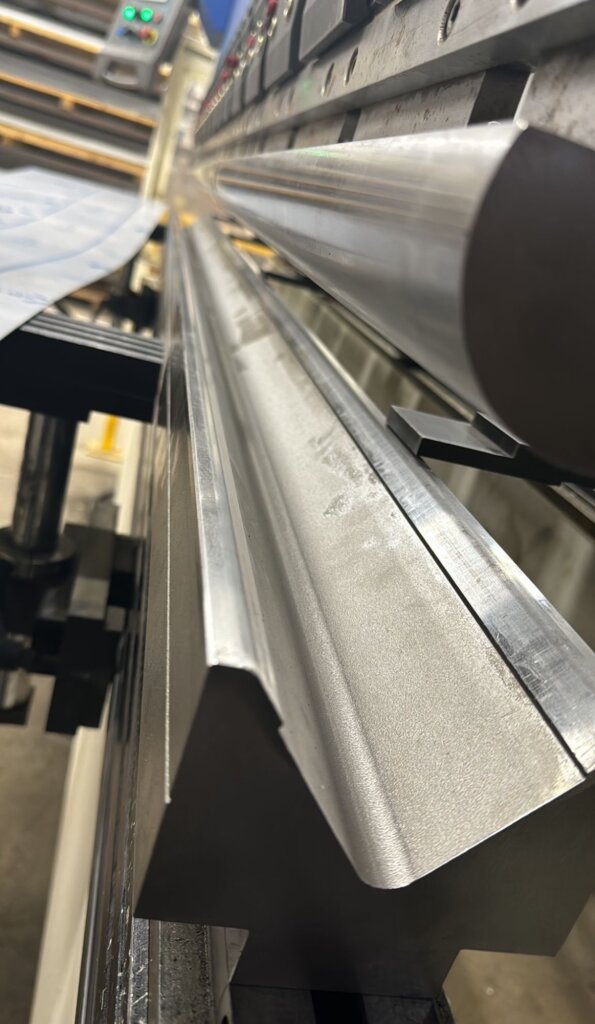
The project encompassed the installation of bespoke hygienic stainless steel kerbing, fabricated in-house by KDH to meet the highest food industry standards. This was seamlessly integrated with a FeRFA-accredited Foodcrete resin flooring system and a new drainage infrastructure designed to EHEDGE standards, all while maintaining full compliance with BRC (British Retail Consortium) standards and British Safety Standards.
Project Execution
Understanding the critical need for uninterrupted production, KDH Projects meticulously planned the refurbishment to align with the client’s operational demands. Our experienced team implemented stringent control measures to ensure that food safety protocols were upheld at every stage. Key elements of the project included:
- Hygienic Stainless Steel Kerbing:
Custom-fabricated in KDH’s workshop, the kerbing was precision-engineered to provide superior durability and hygiene. Designed for seamless integration with the flooring, the kerbing minimizes potential harborage points for bacteria, facilitating easier cleaning and sanitation. - Foodcrete Resin Flooring System:
A FeRFA accredited KDH Flooring team to install Foodcrete resin flooring solution was installed to provide a high-performance, seamless surface that is non-porous, easy to clean, and resistant to heavy foot and FLT vehicle traffic. The flooring successfully passed slip testing to British Safety Standards, ensuring a safe working environment. - EHEDG Compliant Drainage System:
A new drainage system was installed to meet EHEDG guidelines, the system ensures the highest levels of hygiene and compliance. - Working in a Live Production Environment:
As specialists in food factory refurbishments, KDH Projects ensured zero compromise on food safety by implementing controlled work zones, regular hygiene checks, and close collaboration with the client’s technical teams to minimize disruption and maintain compliance with BRC food safety standards.
Challenges and Solutions
Working within a live production facility required strategic planning and coordination to avoid disruption to daily operations. KDH Projects utilized phased work scheduling, ensuring minimal downtime while maintaining strict hygiene controls. Our proactive approach enabled us to adapt to operational constraints without compromising project quality or food safety.
Outcome and Client Benefits
The successful completion of the project delivered:
- A fully compliant, hygienic, and food-safe stores area that meets all regulatory and safety requirements.
- Enhanced durability of flooring and kerbing, reducing future maintenance and operational disruptions with constant FLT and load traffic
- Improved drainage performance, promoting a cleaner and safer working environment.
- Zero food safety incidents during the refurbishment, highlighting KDH’s commitment to high standards and operational excellence.
KDH Projects’ ability to execute high-quality refurbishments within live food production environments underscores our expertise and dedication to food safety, compliance, and customer satisfaction.